Work Performed
Field challenge
The existing tool had no sensor for actual supply flow. Operators could only check chemical pressure on an analog gauge or rely on low/high alarms. Actual flow in the metal-etchant, DI water/rinse and N2/air-knife lines was therefore not visible on the operator screen, and a supply abnormality could affect the etching process. Existing tubing and piping also had to remain as unchanged as possible.
Work / Solution
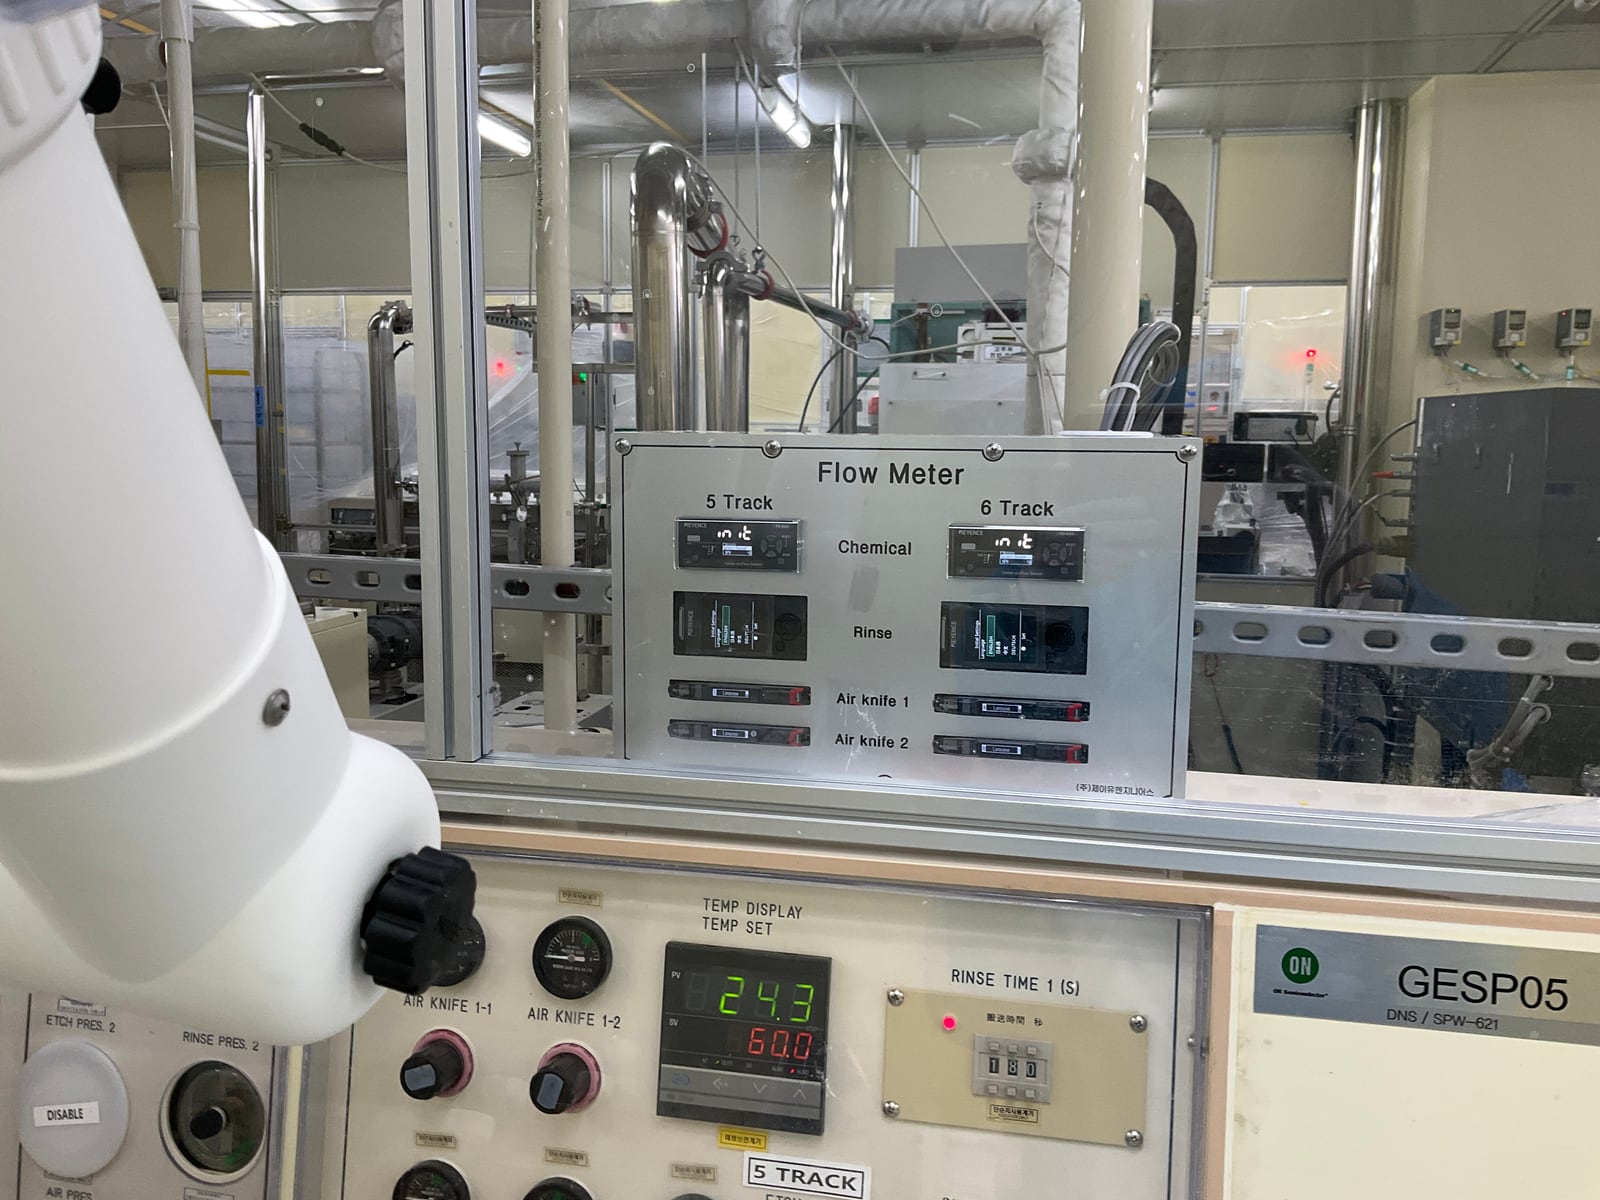
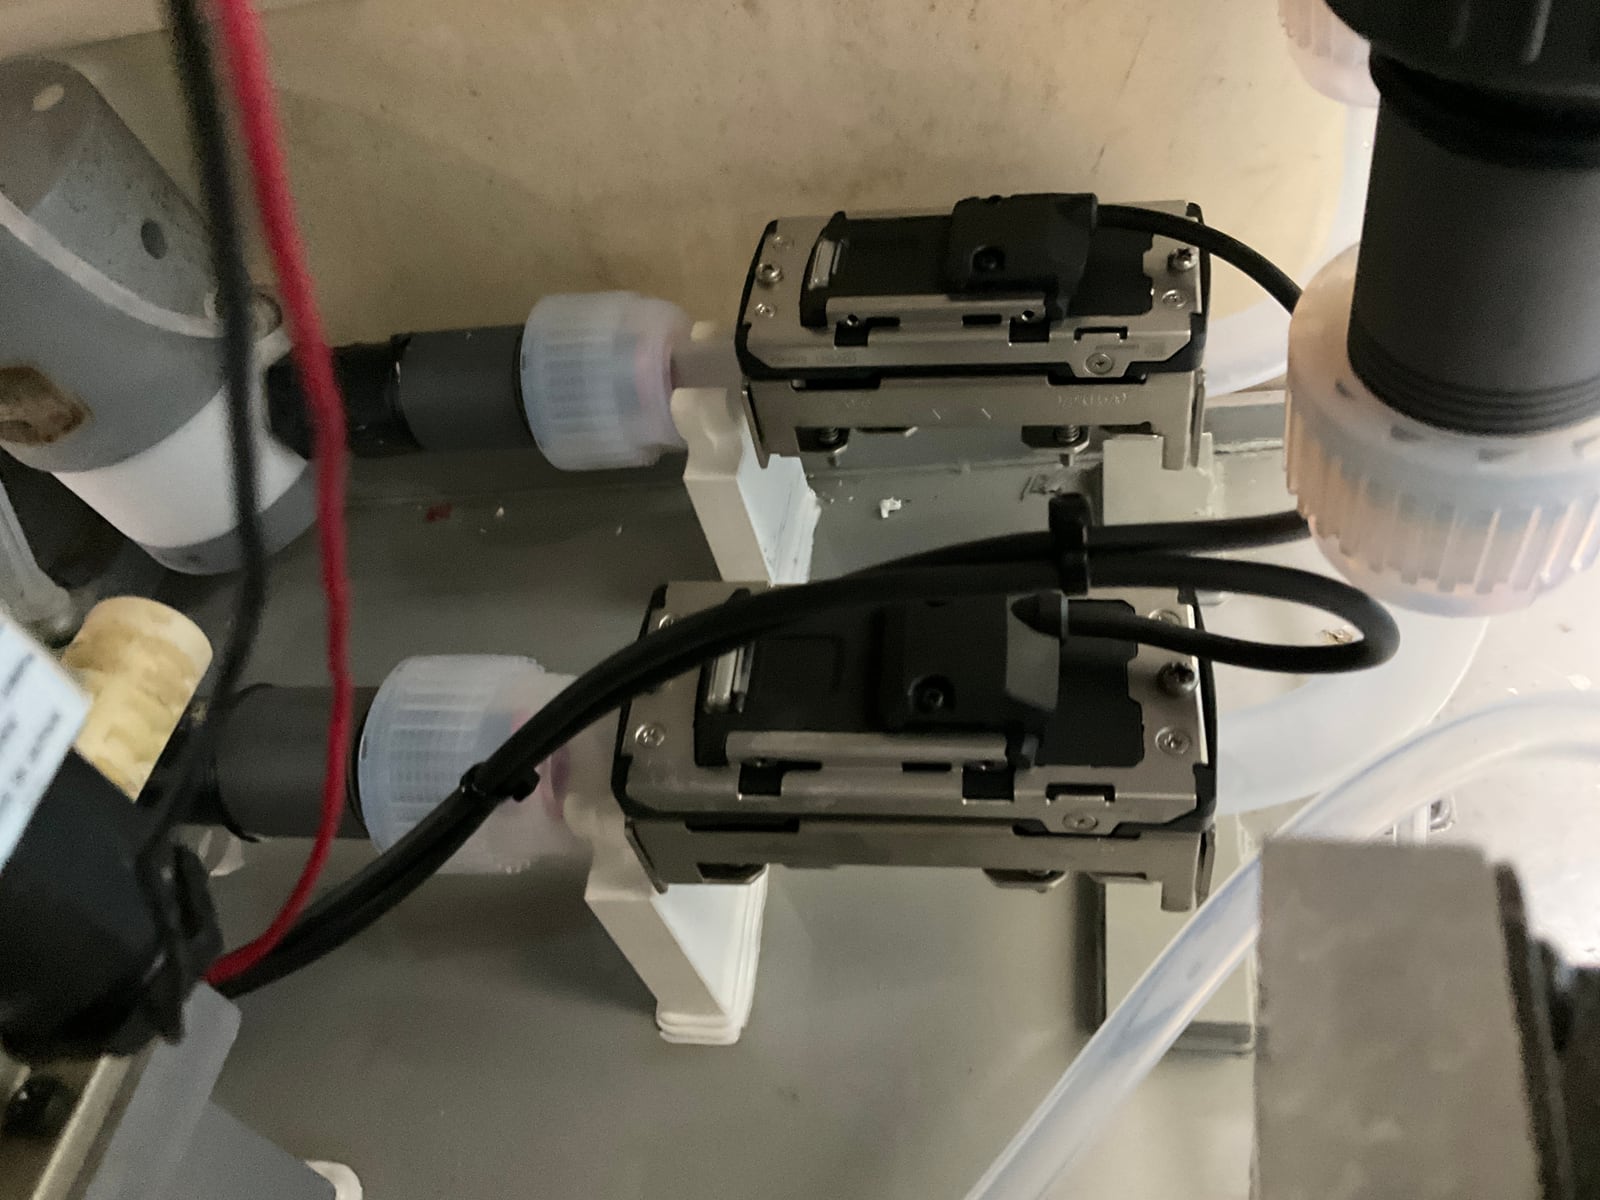
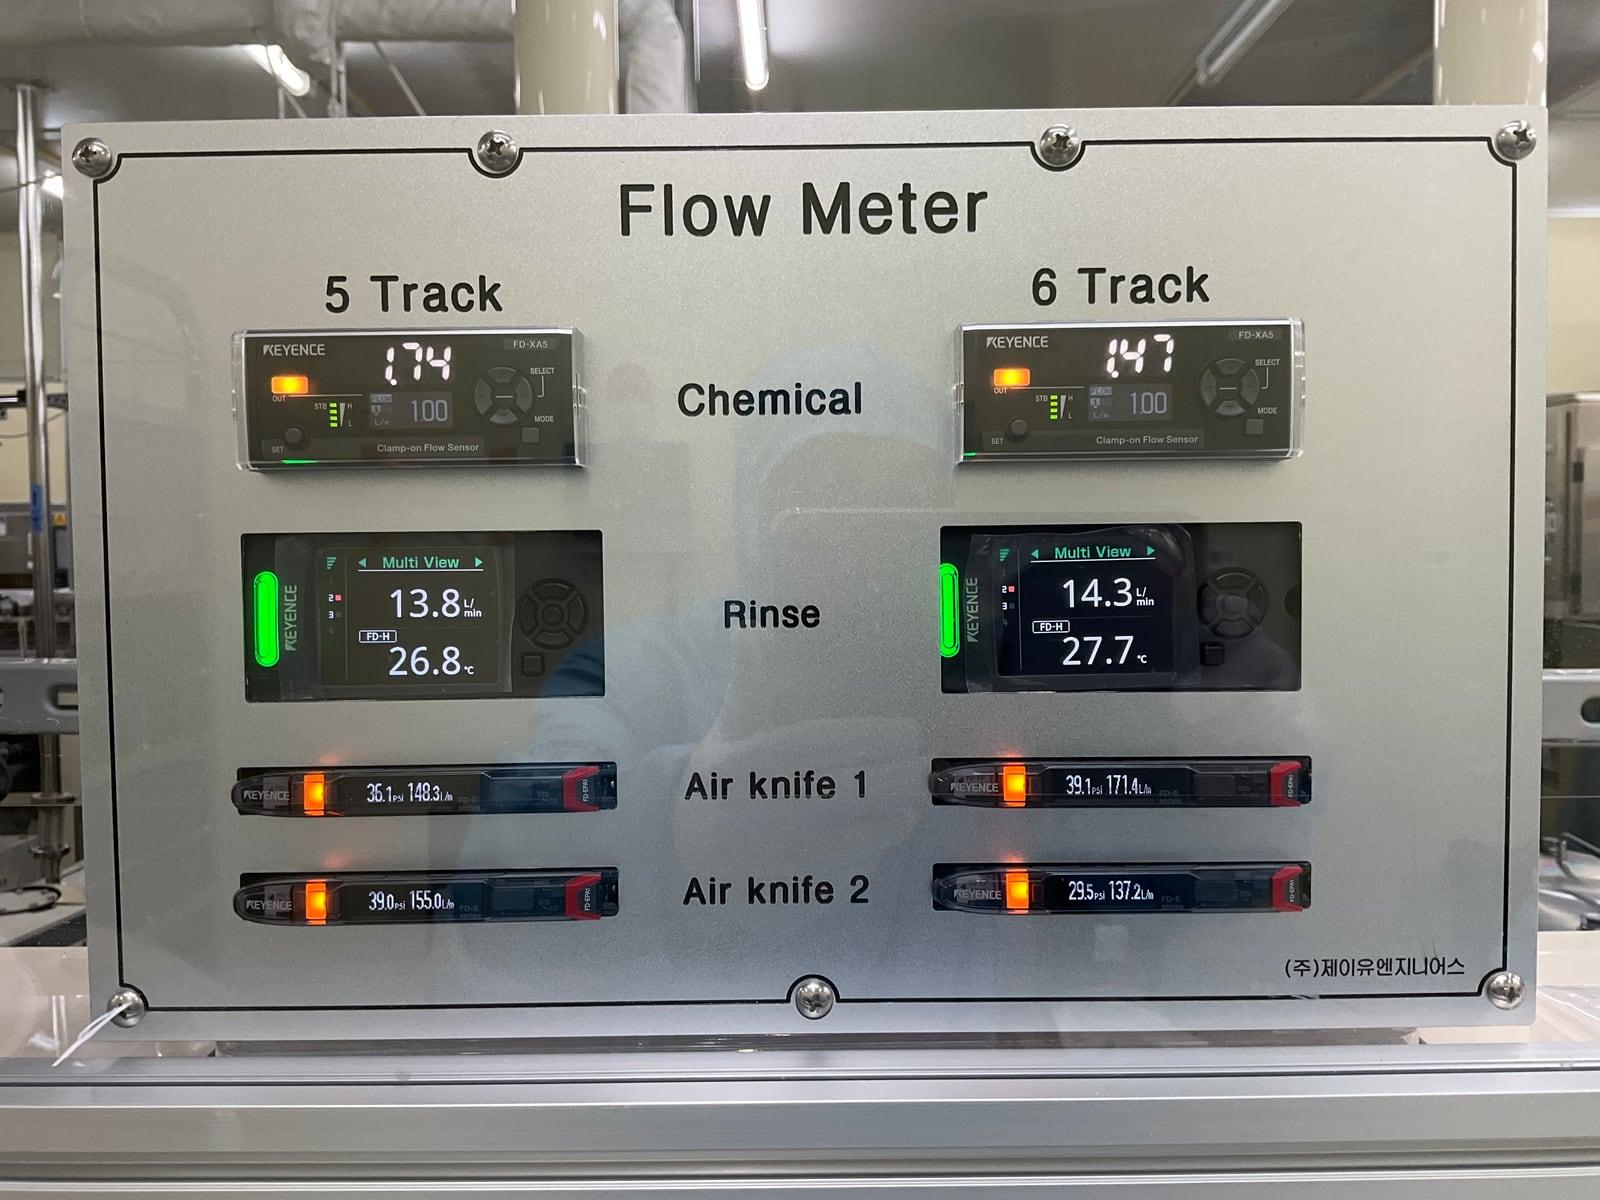
KEYENCE clamp-on flow sensors were installed on the chemical and N2 tubing without cutting the lines. JUNSEMI completed the sensor installation, electrical work, wiring, PLC modifications and touch-panel updates, displaying real-time flow by circuit and linking the measurements to alarms and process interlocks. A watchdog delay issues an alarm only when abnormal flow continues beyond the configured time, filtering brief fluctuation and hunting. When an abnormal condition persists, new process starts are inhibited; a wafer already in process is allowed to rinse and unload through a controlled safe-completion sequence. Operators can configure the flow threshold, delay time and interlock enable setting from the touch panel.
Key functions and engineering
• Flow monitoring for metal etchant, DI water/rinse and N2/air-knife lines
• KEYENCE non-contact clamp-on flow sensors
• Retrofit installation with no tubing cut on the monitored lines
• Sensor wiring, PLC input handling and process-interlock integration
• Watchdog-based persistence check and hunting suppression
• Abnormal-flow alarm and new-process inhibit
• Rinse and unload sequence for a wafer already in process
• Touch-panel settings for threshold, delay and interlock enable
Verified Result
Verified real-time flow display, time-qualified alarms, new-process inhibition, rinse-and-unload handling for an in-process wafer and the operator settings together with the customer. No numerical defect-reduction rate is claimed because quantified data was not available.
Field Photos